In today’s fast-paced industrial landscape, efficient material handling systems are essential for productivity, safety, and cost optimization. Businesses across sectors such as mining, packaging, food processing, logistics, and manufacturing rely heavily on robust conveyor solutions to streamline operations. Choosing the right belt conveyor manufacturer in united states can make a significant difference in operational efficiency and long-term profitability.
Among the trusted names in this domain, Samarth Engineerings stands out for delivering high-performance conveyor systems tailored to diverse industrial requirements. With a strong commitment to innovation, quality, and customization, the company continues to support industries in achieving seamless material flow and enhanced productivity.
Why Belt Conveyors Are Essential in Modern Industries
Belt conveyors are the backbone of material handling systems. They offer a reliable, cost-effective, and scalable solution for transporting goods across various distances and environments.
Key Advantages of Belt Conveyors
- Efficiency Boost: Automates material movement, reducing manual labor
- Cost-Effective: Low operational and maintenance costs
- Versatility: Suitable for a wide range of materials and industries
- Safety Enhancement: Minimizes workplace injuries
- Scalability: Easily adaptable to growing production needs
Industries today demand precision-engineered systems that can handle heavy loads, operate continuously, and withstand harsh conditions. This is where an experienced belt conveyor manufacturer in united states plays a vital role.
About Samarth Engineerings
Samarth Engineerings has built a strong reputation for designing and manufacturing high-quality conveyor systems that meet global standards. The company focuses on delivering durable, efficient, and customized solutions that cater to specific industry needs.
With a customer-centric approach, Samarth Engineerings ensures that every product is engineered with precision and tested for performance. Their expertise spans across multiple industries, making them a preferred partner for businesses seeking reliable conveyor solutions.
Core Strengths
- Advanced engineering capabilities
- Custom design solutions
- High-quality materials and components
- Timely project delivery
- Competitive pricing
High-Performance Conveyor Solutions Offered
Samarth Engineerings provides a wide range of conveyor systems designed to meet different operational requirements. Their solutions are known for durability, efficiency, and adaptability.
1. Industrial Belt Conveyors
Designed for heavy-duty operations, these conveyors are ideal for industries like mining, cement, and bulk material handling.
Features:
- High load-bearing capacity
- Abrasion-resistant belts
- Long service life
- Minimal maintenance
2. Modular Belt Conveyors
Perfect for industries requiring flexibility and easy reconfiguration.
Benefits:
- Easy installation and modification
- Suitable for complex layouts
- Reduced downtime
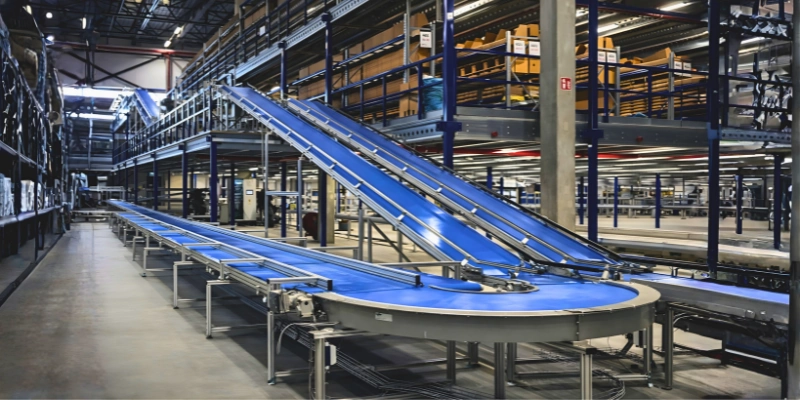
3. Inclined and Declined Conveyors
Used for transporting materials between different elevations.
Advantages:
- Space optimization
- Smooth material transfer
- Enhanced operational efficiency
4. Customized Conveyor Systems
Samarth Engineerings specializes in creating tailor-made solutions to match specific business needs.
What Makes a Reliable Belt Conveyor Manufacturer?
Selecting the right partner is crucial when investing in conveyor systems. Not all manufacturers offer the same level of expertise, quality, and service.
Key Factors to Consider
1. Engineering Expertise
A reputable belt conveyor manufacturer in united states should have a strong technical foundation and experience in handling diverse projects.
2. Customization Capabilities
Every industry has unique requirements. The ability to customize solutions ensures better performance and efficiency.
3. Quality Standards
High-grade materials and strict quality control processes are essential for long-lasting conveyor systems.
4. After-Sales Support
Reliable maintenance and support services help in minimizing downtime and extending equipment life.
5. Innovation and Technology
Modern conveyor systems should incorporate advanced technologies for improved efficiency and automation.
Industries Served
Samarth Engineerings caters to a wide range of industries, providing solutions that improve productivity and streamline operations.
Major Industries Include:
- Manufacturing – Assembly lines and production units
- Food Processing – Hygienic and efficient material handling
- Mining & Minerals – Heavy-duty conveyor systems
- Logistics & Warehousing – Fast and reliable goods movement
- Packaging Industry – Smooth product flow and sorting
Their ability to adapt to different industry requirements makes them a versatile and dependable partner.
Commitment to Quality and Innovation
One of the defining aspects of Samarth Engineerings is its unwavering commitment to quality and innovation. The company continuously invests in research and development to enhance product performance and meet evolving industry demands.
Quality Assurance Practices
- Rigorous testing procedures
- Compliance with international standards
- Use of premium-grade materials
- Continuous process improvement
By focusing on innovation, Samarth Engineerings ensures that its conveyor systems remain efficient, reliable, and future-ready.
Benefits of Partnering with Samarth Engineerings
Choosing the right manufacturer goes beyond just purchasing equipment—it’s about building a long-term partnership.
Why Choose Samarth Engineerings?
- Tailored Solutions: Customized designs to meet specific needs
- High Performance: Efficient systems that boost productivity
- Durability: Long-lasting and robust conveyor systems
- Expert Support: Dedicated technical assistance
- Timely Delivery: Projects completed within deadlines
Businesses looking to upgrade their material handling systems can confidently explore solutions and collaborate with Samarth Engineerings to achieve operational excellence.
Future of Conveyor Systems in the USA
The demand for advanced conveyor systems is rapidly increasing due to automation and Industry 4.0 trends. Companies are seeking smarter, more efficient solutions that integrate seamlessly with modern technologies.
Emerging Trends
- Automation and smart conveyor systems
- Energy-efficient designs
- Integration with IoT and AI
- Enhanced safety features
A forward-thinking belt conveyor manufacturer in united states must stay ahead of these trends to deliver innovative solutions that meet future demands.
Final Thoughts
Investing in high-performance conveyor systems is essential for businesses aiming to improve efficiency, reduce costs, and stay competitive in today’s dynamic market. Choosing a reliable belt conveyor manufacturer in united states ensures that you get durable, efficient, and customized solutions tailored to your needs.
With its strong engineering expertise, commitment to quality, and customer-focused approach, Samarth Engineerings continues to be a trusted name in the industry. Whether you need standard conveyor systems or fully customized solutions, their offerings are designed to deliver performance, reliability, and long-term value.
If you’re planning to enhance your material handling operations, now is the time to act and explore innovative conveyor solutions that can transform your business operations.