In today’s fast-paced industrial environment, efficient material movement is essential for productivity, safety, and cost control. This is why belt conveyors manufacturers play a critical role across industries such as manufacturing, warehousing, mining, food processing, logistics, and packaging. Belt conveyors provide a continuous, reliable, and automated way to transport materials over short or long distances with minimal manual effort.As industries in India continue to modernize, demand for robust and customized belt conveyor systems is growing rapidly.
What Are Belt Conveyors?A belt conveyor is a mechanical handling system that uses a continuous belt loop to move materials from one point to another. The belt runs over pulleys and is supported by rollers or a solid bed, allowing smooth transportation of goods such as cartons, bags, bulk materials, components, and finished products.Reputed belt conveyors manufacturers design these systems to handle different load capacities, operating conditions, and layouts, making them suitable for both light-duty and heavy-duty applications.
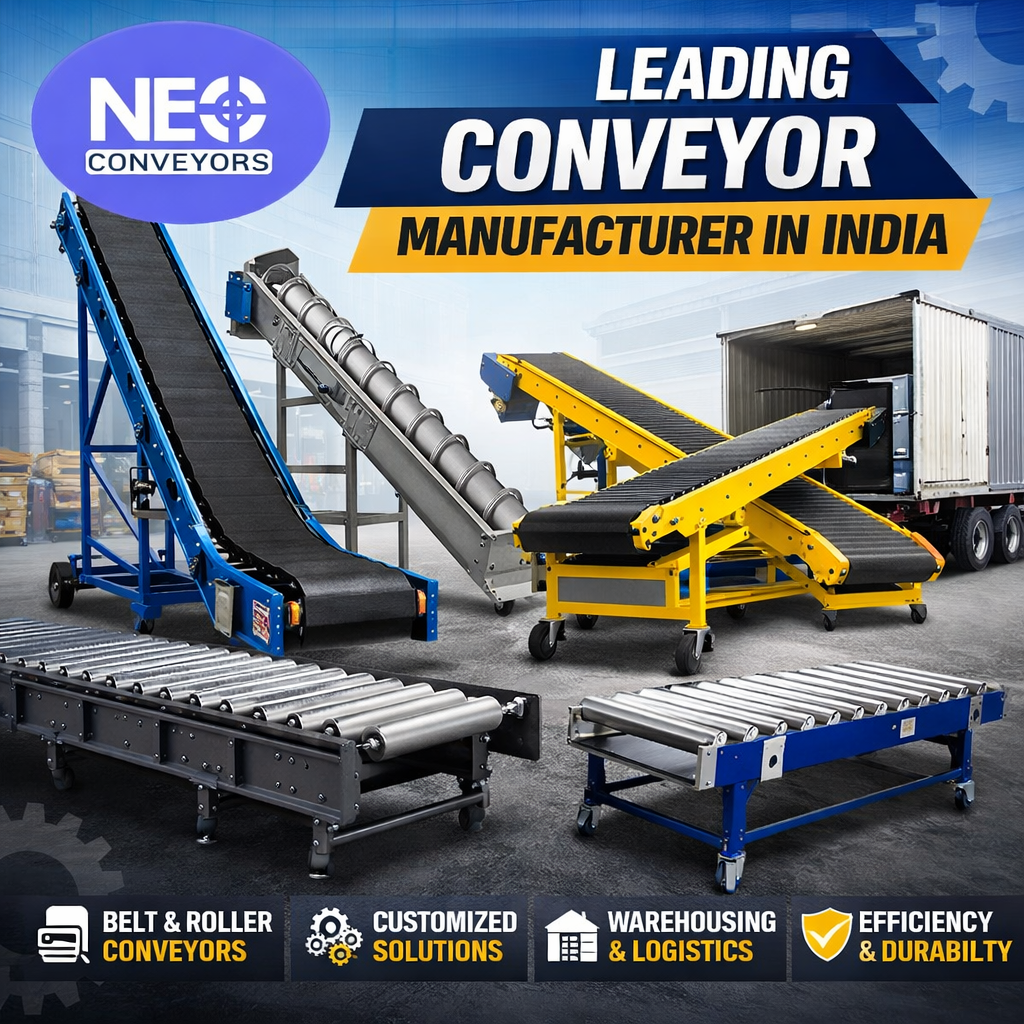
Types of Belt Conveyors Used in IndustryProfessional belt conveyors manufacturers offer a wide range of conveyor designs to meet diverse industrial needs:
1. Flat Belt ConveyorsIdeal for transporting boxes, packages, and unit loads in warehouses and assembly lines.
2. Inclined Belt ConveyorsDesigned to move materials between different heights with cleats or sidewalls to prevent slippage.
3. Trough Belt ConveyorsCommonly used for bulk material handling such as sand, coal, grains, and minerals.
4. Slider Bed & Roller Bed Belt ConveyorsUsed where smooth, stable movement and higher load capacities are required.
5. Telescopic & Portable Belt ConveyorsWidely used in logistics and truck loading/unloading operations for flexibility and speed.Each type is engineered with specific belts, frames, motors, and controls to ensure durability and efficiency.
Key Benefits of Belt Conveyor SystemsWorking with experienced belt conveyors manufacturers ensures several operational advantages:Increased productivity through continuous material flowReduced manual labor and handling costsImproved workplace safetyConsistent and damage-free product movementCustomizable layouts to suit available spaceEnergy-efficient operation with low maintenance needsThese benefits make belt conveyors an essential investment for growing businesses.
Applications Across IndustriesBelt conveyors are used across a wide range of sectors, including:Manufacturing & assembly plantsWarehouses & distribution centersFood & beverage processing unitsCement, mining, and power plantsFMCG and packaging industriesAirports, courier hubs, and logistics facilitiesLeading belt conveyors manufacturers customize systems to meet industry-specific standards, load requirements, and environmental conditions.How to Choose the Right Belt Conveyors ManufacturerSelecting the right manufacturer is just as important as choosing the conveyor itself. When evaluating belt conveyors manufacturers, consider the following factors:Experience and industry expertiseAbility to offer customized solutionsQuality of materials and components usedIn-house design and manufacturing capabilitiesInstallation, testing, and after-sales supportCompliance with safety and quality standardsA reliable manufacturer will focus on long-term performance rather than just initial cost.
Why Neo Conveyors Is a Trusted Name in IndiaNeo Conveyors is one of India’s leading belt conveyors manufacturers, offering engineered solutions for a wide range of industrial applications. With years of experience in material handling systems, the company designs and manufactures durable, high-performance belt conveyors tailored to customer requirements.Neo Conveyors provides flat belt conveyors, inclined conveyors, trough belt conveyors, and customized belt conveyor systems using high-quality components and advanced engineering practices. Their solutions are known for reliability, efficiency, and long service life.To explore their belt conveyor solutions in detail, visit:Belt Conveyor Systems by Neo ConveyorsContact our support team at [email protected] call +91 9654112236.
ConclusionAs industries continue to automate and scale operations, the role of belt conveyors manufacturers becomes increasingly important. A well-designed belt conveyor system improves productivity, reduces operational bottlenecks, and enhances workplace safety.By partnering with an experienced manufacturer like Neo Conveyors, businesses can ensure they receive customized, efficient, and future-ready material handling solutions that support long-term growth.
35 Просмотры